

Regenerative Thermal Oxidizer (RTO) for Landfill Gas Treatment
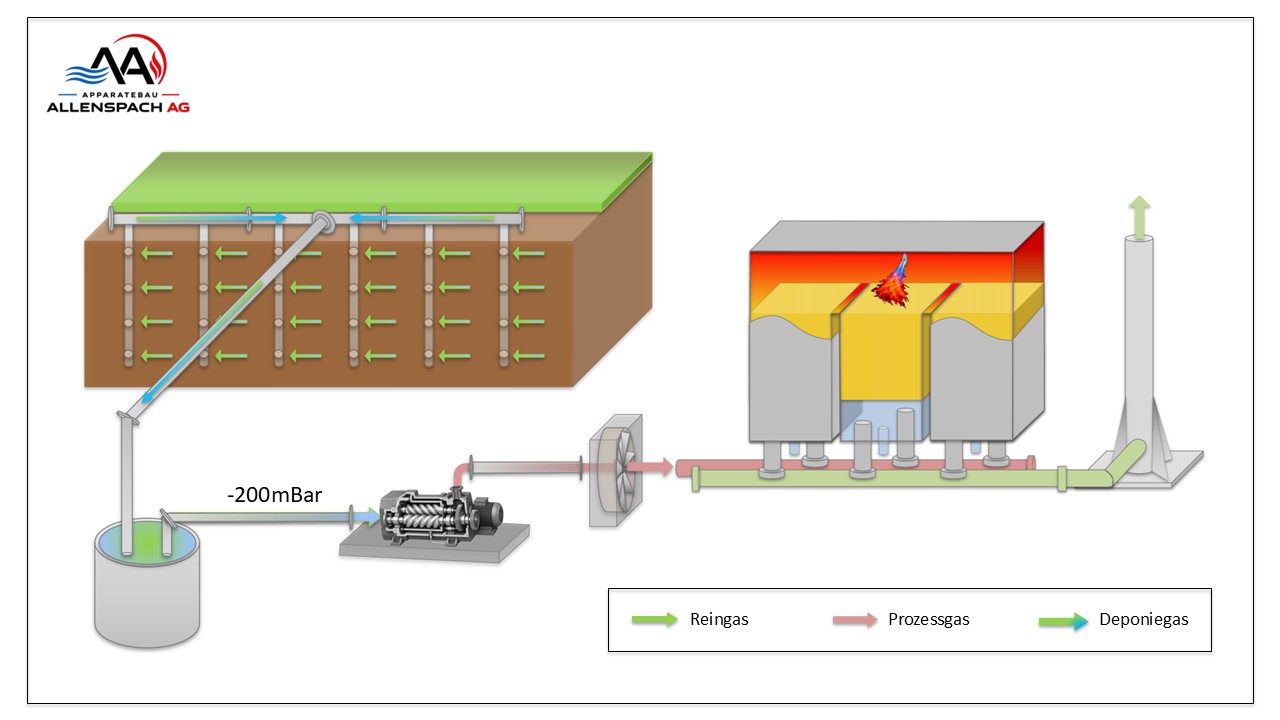
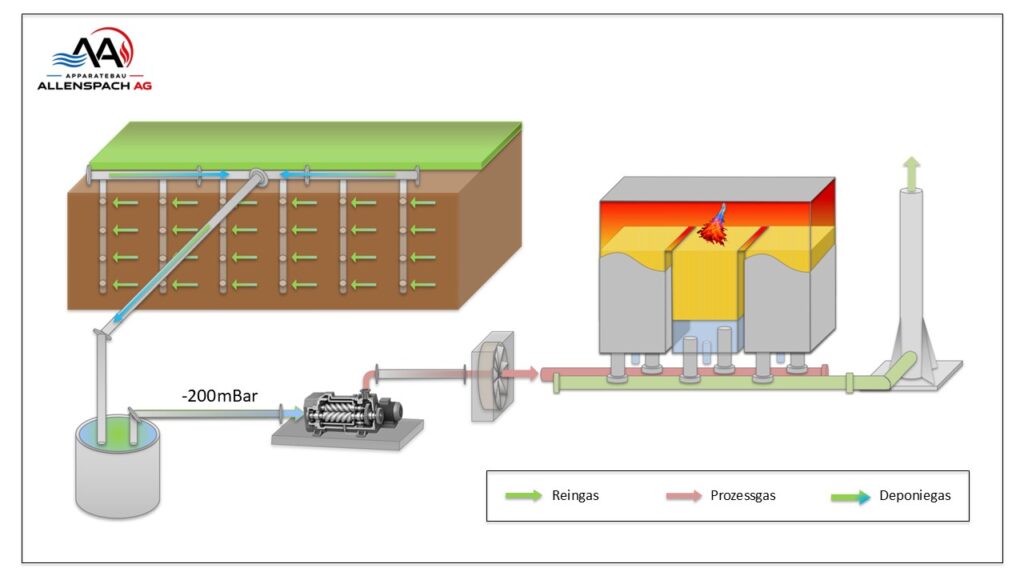
The landfill gas is continuously conveyed to the RTO system via the collection network by means of a vacuum generated by a compressor and is thermally treated there under controlled conditions.
The system converts captured methane mainly to CO₂ and water, reducing the climate impact of methane emissions. Performance is assessed for the landfill gas composition and operating conditions.
Auxiliary energy for start-up is provided electrically. Thanks to the energy-efficient plant design and regenerative heat recovery, the plant can operate autothermally after start-up at sufficient methane concentration and flow. Additional heating may be required during low-load or transient conditions. This significantly reduces both energy consumption and operating costs.
Features of the RTO Landfill Gas Plant
- Thermal oxidation of methane and other organic components
- Oxidation temperature selected for gas composition, residence time and emissions target; verified operating range for this project: 820–950 °C
- Ceramic heat storage media with high thermal efficiency
- Landfill gas extraction by compressor at the project-specific suction pressure (up to approx. 200 mbar below ambient pressure)
- Electrical heating as auxiliary energy
- 3-chamber system with integrated purge cycle for emission minimization
- Compliance with statutory emission limit values
- High operational reliability and fully automatic process control
- Autothermal operation with sufficient methane concentration
- Regulated hot gas bypass for temperature and energy limitation